






Carcaça Automotiva Personalizada Leve para Veículos Elétricos: Materiais e Estratégias de Design
Para eletrônica de veículos elétricos, Reduzir o peso da carcaça raramente é um exercício simples de substituição de material. Uma carcaça automotiva personalizada deve proteger a eletrônica, manter a estabilidade dimensional, dissipar calor, resistir à vibração e à corrosão, Vedação de suporte, e—quando necessário—fornecer blindagem EMI.
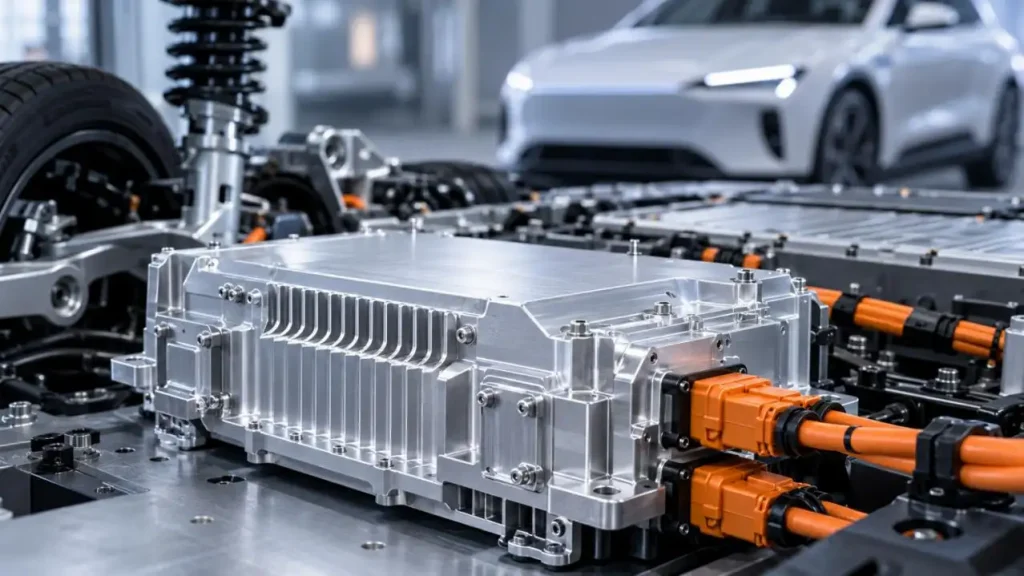
Do ponto de vista da manufatura, A questão principal não é simplesmente "Quão leve pode ser a carcaça?" mas sim:
How much material can be removed without compromising stiffness, Desempenho térmico, sealing integrity, machining stability, or production repeatability?
Na GD Prototipagem, this is the point where material selection, DFM, Estratégia de usinagem, and prototype validation need to be considered together.
What Defines a Lightweight Custom Automotive Housing?
A Custom Automotive Housing is engineered around a specific ECU, sensor, inverter, controller, charging module, or ADAS device. Unlike a standard enclosure, its geometry is typically driven by several functional requirements at the same time:
•Mechanical protection and mounting stiffness
• Heat transfer from internal electronics
• EMI/EMC performance
• IP-rated sealing interfaces
• Connector and cable positioning
• Vibration and thermal-cycle resistance
• Weight and package-space targets
• Manufacturing process and production volume
For EV applications, these requirements often conflict. Thinner walls reduce mass, por exemplo, but also increase the risk of machining distortion, local vibration, sealing-surface deformation, and reduced thread engagement.
That is why lightweight Custom Automotive Housing design should be treated as a system-level optimization problem.
Seleção de Material: Alumínio, Plastic or Composite?
There is no universal "melhor" material. The correct choice depends on the dominant engineering constraint.
| Material | Principais Vantagens | Main Design Concerns | Aplicações Típicas |
| 6061-T6 Aluminum | Good strength-to-weight ratio, Usinabilidade, Condutividade térmica, Resistência à corrosão | Distorção de parede fina, machining cost at scale | Sensores, Controladores, Cároles da ECU |
| Die-Cast Aluminum | Geometria complexa, integrated ribs and bosses, Produção escalável | Custo de ferramentas, draft and wall-thickness constraints | Inverters, Módulos de controle |
| Plásticos de Engenharia | Baixa massa, Isolamento elétrico, molded feature integration | Condutividade térmica, Blindagem EMI, rastejar | Sensor and electronic enclosures |
| Fiber-Reinforced Polymers | Higher stiffness than standard plastics, Baixa densidade | Anisotropy, ferramental, thermal/EMI limitations | Structural lightweight housings |
| Ligas de Magnésio | Very low density | Proteção contra corrosão, Controle de processos, custar | Weight-critical applications |
For many precision EV electronics, aluminum remains attractive because one Custom Automotive Housing can perform several functions simultaneously: structural enclosure, heat spreader, mounting frame, and EMI shield.
Seven Design Decisions That Control Housing Weight
1. Espessura da parede
Wall thickness should be based on unsupported span, load path, sealing pressure, vibration environment, and manufacturing method—not on a single minimum value.
For CNC-machined aluminum housings, aggressive wall reduction can create:
• Deflection during machining
• Chatter and poor surface finish
• Bore or pocket distortion
• Flatness changes after unclamping
• Dimensional drift during anodizing or thermal cycling
2. Ribs Instead of Bulk Material
Localized increases in wall thickness through the use of ribs increase stiffness more effectively than using a uniform increase in wall thickness.
Particularly effective use of ribs is in:
• Ear locations
• Connector zones
• Bore locations of bearings and sensors
• Large, unsupported, Painéis
• Screw bosses and sealing flanges
3. Functional Integration
Design of a lightweight Custom Automotive Housing should integrate, sempre que possível, secondary functions to eliminate the need for other, separate, components.
Cable interfaces and mounting bosses should be integrated on the housing along with internal supports and cooling fins.
Integrating these features results in a reduction of both the number of components and the overall weight of the housing.
4. Gestão Térmica
For power electronics, weight reduction must not interrupt the thermal path.
Important design questions include:
• Where is heat generated?
• Is the housing acting as a heat spreader?
• Is there sufficient contact area for TIM materials?
• Are fins or cooling channels required?
• Will thin walls create local hot spots?
In many EV applications, thermal performance sets the practical lower limit for housing thickness.
5. EMI and EMC Performance
Shielding can limit the amount of EMI and EMC a device can transmit, but the use of seals and gaskets can diminish a housing's shielding ability.
When a housing must block high frequency or high voltage energy, shielding must be designed into the housing in order to be effective.
6. Sealing and Environmental Protection
The flange shape of an IP-rated housing is determined by the sealing element.
When designing a housing, various elements such as...
• Compression of the gasket
• Dims of a gasket groove
• Flatness of the flange
• Spacing of the fasteners
• The material being fastened
• The thickness of a coating
• May impact the effectiveness of the sealing element.
Removing material to thin the part can negatively impact the part, and affect the compression of a sealing element.
7. Processo de Fabricação
The geometry of a Custom Automotive Housing should reflect its production route.
| Processo | Best Use | Design Implication |
| Usinagem CNC de 5 Eixos | Prototype and low-volume precision housings | Allows tight tolerances and frequent design changes |
| O Elenco | Medium/high-volume aluminum housings | Requires draft, uniform walls, tooling strategy |
| Moldagem por Injeção | Plastic housings at production scale | Requires flow, Costelas, Chefes, shrinkage control |
| Impressão 3D | Early concept and fit validation | Useful before committing to production geometry |
| Fundição a vácuo | Small-batch functional evaluation | Suitable for limited-volume polymer parts |
GD Prototyping Case: Thin-Wall Automotive Sensor Housing
A useful example is a precision aluminum sensor housing produced by GD Prototyping using 5-axis CNC machining.
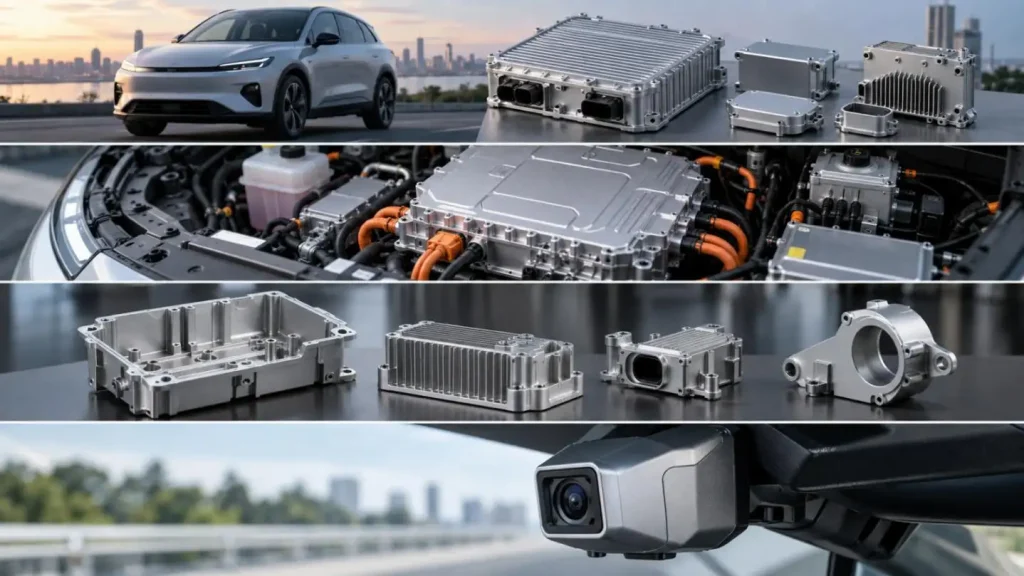
The component specifications included:
• Material: 6061-T6 aluminum
• Part size: 87 × 54 × 32 mm
• Espessura mínima da parede: 1,2 mm
• Critical bore: Ø22 mm
• Critical tolerance: ±0.01 mm
• Acabamento superficial do diâmetro: Ra 0,8 μm
• Acabamento superficial externo: Ra 1,6 μm
• Surface treatment: Anodização Tipo II, 15 μm ±2 μm
• Production quantity: 150 units
The challenge was not simply removing material. At 1.2 mm wall thickness, Força de fixação, toolpath sequence, cutting load, temperatura, and inspection strategy all influenced final dimensional stability.
The production approach used dedicated fixturing, controlled machining sequences, Estabilização térmica, and CMM inspection. GD Prototyping reported a 99.3% first-pass yield for the batch.
This illustrates an important principle for any lightweight Custom Automotive Housing:
As the housing becomes lighter, manufacturing process control becomes more—not less—important.
DFM Checklist for Custom Automotive Housing
Before releasing a housing design for prototyping, we recommend reviewing the following:
• Are wall thicknesses consistent with stiffness requirements?
• Are tight tolerances limited to functional features?
• Can all critical surfaces be machined and inspected?
• Are sealing flanges sufficiently rigid?
• Are heat paths clearly defined?
• Are EMI requirements reflected in material and finish?
• Can ribs replace unnecessary solid material?
• Will anodizing or coating affect critical dimensions?
• Is the design intended for CNC, fundição, or molding?
• Is the production volume high enough to justify hard tooling?
These decisions often have more impact on cost and reliability than the nominal material choice.
Considerações Finais
A successful lightweight Custom Automotive Housing is not the lightest possible enclosure. It is the lightest design that still satisfies structural, termal, EMC, vedação, Dimensional, and manufacturing requirements.
For early-stage EV electronics, CNC machining is often valuable because engineers can validate real aluminum parts before committing to die-casting or injection-molding tooling.
GD Prototyping supports 3-, 4-, e usinagem CNC de 5 eixos, Torneamento CNC, Impressão 3D, Fundição a vácuo, Moldagem por injeção, sheet-metal fabrication, e fundição sob pressão, allowing a Custom Automotive Housing project to move from prototype validation toward low-volume or production manufacturing without treating each stage as an isolated process.
If your housing design is still being optimized for wall thickness, Tolerâncias, material, vedação, or production method, GD Prototyping can review the CAD data from a manufacturing perspective and help identify practical DFM risks before tooling or production decisions are finalized.
Perguntas frequentes
Q1. Can GD Prototyping manufacture Custom Automotive Housing?
Sim. GD Prototyping manufactures Custom Automotive Housing for prototypes and low-volume production using CNC machining, O Elenco, Moldagem por injeção, Impressão 3D, Fundição a vácuo, e fabricação de chapa metálica.
Q2. What materials are available for Custom Automotive Housing?
GD Prototyping works with metals such as aluminum, aço, e titânio, as well as plastics including ABS, Computador pessoal, POM, e PMMA. Material selection depends on weight, força, termal, EMI, and production requirements.
Q3. Is 5-axis CNC machining suitable for automotive housings?
Sim. 5-axis CNC machining is suitable for complex Custom Automotive Housing with deep pockets, multiple mounting surfaces, Furos de Precisão, and features that would otherwise require several setups. A prototipagem GD fornece 3 eixos, 3 2-eixos, and full 5-axis machining.
Q4. What tolerances can GD Prototyping achieve on automotive housings?
Tolerance depends on geometry and material. In one automotive sensor housing project, GD Prototyping held a ±0.01 mm bore tolerance on 6061-T6 aluminum parts with 1.2 mm minimum wall sections.
Q5. Can GD Prototyping machine thin-wall Custom Automotive Housing?
Sim. A published automotive project involved a 6061-T6 aluminum housing measuring 87 × 54 × 32 mm with 1.2 mm thin-wall sections, produced using 5-axis CNC machining.
